Pasteurizers & sterilizers · · 5 min read
Milk Pasteurizer Buying Guide: Plate, Tubular, Batch or UHT
Compare HTST plate, tubular, batch and UHT milk pasteurizers: time-temperature rules, regeneration, shelf life and a step-by-step checklist for buyers.
By the process engineering team at Shanghai Mars Industrial Co., Ltd.
Key takeaways
- HTST pasteurization of milk means at least 72 °C for 15 seconds; batch (vat) pasteurization means at least 63 °C for 30 minutes.
- Plate heat exchangers suit low-viscosity milk and recover up to 94–95% of heat; tubular units tolerate particles, pulp and higher pressures.
- UHT treatment runs at 135–150 °C for a few seconds and, with aseptic filling, gives months of ambient shelf life.
- Size the pasteurizer from real hourly flow, holding-tube length and the cleaning cycle, not from the daily milk volume alone.
Which milk pasteurizer should you choose?
Choose an HTST plate pasteurizer for continuous fresh milk above a few thousand litres per day, a batch (vat) pasteurizer for small or multi-product runs, a tubular unit for viscous or particulate products, and a UHT system with aseptic filling when you need months of ambient shelf life. The deciding factors are product type, hourly flow, target shelf life and budget for downstream packaging.
All four technologies destroy pathogens; they differ in how fast heat is transferred, how much energy is recovered, what the product looks and tastes like afterwards, and how long it keeps. This guide compares them with verified time–temperature standards and gives a practical selection checklist.
What time and temperature does milk pasteurization require?
The internationally recognized minimums are 72 °C for 15 seconds for continuous-flow (HTST) pasteurization and 63 °C for 30 minutes for batch pasteurization. The Codex Code of Hygienic Practice for Milk sets these as equivalent minimums, and the US Pasteurized Milk Ordinance adds 3 °C for products with 10% or more fat or added sweeteners.
| Method | Temperature | Minimum time | Typical equipment |
|---|---|---|---|
| Vat / batch (LTLT) | 63 °C (145 °F) | 30 minutes | Jacketed tank with agitator |
| HTST | 72 °C (161 °F) | 15 seconds | Plate or tubular heat exchanger with holding tube |
| HHST | 89–100 °C | 1.0–0.01 seconds | Plate or tubular, higher-pressure design |
| Ultra-pasteurized (UP) | 138 °C (280 °F) | 2 seconds | Tubular, plate or direct steam |
| UHT (Codex) | 135–150 °C | Seconds, to commercial sterility | Indirect tubular/plate or direct steam injection/infusion, plus aseptic filler |
In practice, processors run slightly above the legal floor. The Tetra Pak Dairy Processing Handbook gives 72–75 °C for 15–20 seconds for homogenized market milk, and Codex sets a higher minimum of 75 °C for 15 seconds for cream. Yogurt milk is deliberately heated much harder, typically 90–95 °C for about 5 minutes, to denature whey proteins and improve texture.
How do plate, tubular, batch and UHT pasteurizers compare?
Plate HTST units give the best heat recovery and smallest footprint for liquid milk; tubular units trade some efficiency for tolerance of viscosity, particles and high pressure; batch vats are cheapest and most flexible but slow and energy-intensive; UHT systems cost the most but remove the cold chain.
| Criterion | HTST plate | HTST / UHT tubular | Batch vat | UHT + aseptic |
|---|---|---|---|---|
| Operation | Continuous | Continuous | Batch | Continuous |
| Heat recovery | Up to 94–95% regeneration | High, slightly below plate | Little or none | High (indirect); lower (direct) |
| Best products | Milk, skim, cream up to moderate viscosity | Flavoured milk, cream, drinks with pulp or particles | Small runs, cheese and yogurt milk, pilots | Long-life milk, plant-based drinks, cream |
| Particle tolerance | Low | Monotube designs pass particles up to about 50 mm | High | Depends on heat exchanger |
| Typical shelf life | 7–10 days at 5–7 °C | Same as HTST, or months if UHT | Similar to HTST | Months at ambient (e.g. 3–9 months) |
| Relative cost | Medium | Medium–high | Low | High (includes aseptic filling) |
HTST plate pasteurizers
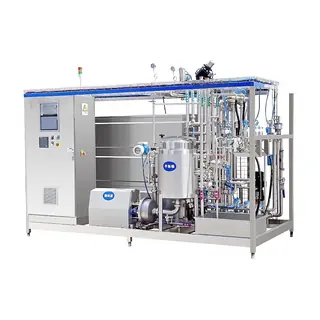
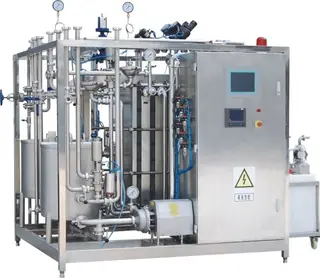
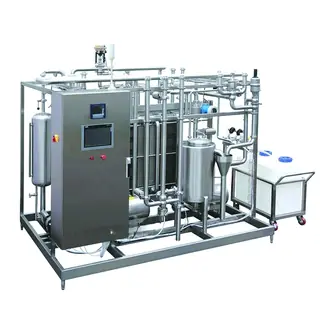
A plate pasteurizer heats milk in thin channels between gasketed plates. Incoming cold milk is warmed by outgoing pasteurized milk in the regeneration section, which, according to the Dairy Processing Handbook, can recycle 94–95% of the heat. A holding tube guarantees residence time, a flow diversion valve returns under-temperature milk to the balance tank, and a booster pump keeps the pasteurized side at higher pressure than the raw side so a pinhole leak cannot contaminate finished milk.
Tubular heat exchangers
Tubular units have fewer gaskets, withstand higher pressures and temperatures, and allow particles to pass. They are the usual choice for indirect UHT, for products with fruit pieces or high viscosity, and for long production runs where fouling would quickly block narrow plate channels.
Batch (vat) pasteurizers
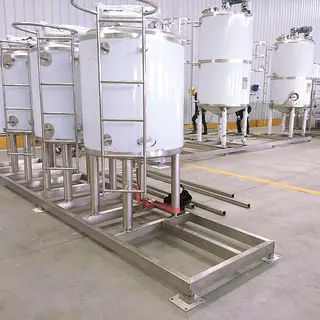
A jacketed, agitated tank holds milk at 63 °C for 30 minutes. It suits small creameries, farmstead cheese makers and plants that switch between many recipes. The drawbacks are long cycle times, little heat recovery and the need for careful temperature recording across the whole vat, including foam and air space.
UHT systems
UHT heats product to 135–150 °C for a few seconds. The handbook describes practical settings of 137–142 °C for 4–6 seconds; indirect tubular plants typically heat to about 138 °C with about 4 seconds' hold, while direct steam injection reaches 140–150 °C and flash-cools in a vacuum vessel. UHT only delivers ambient shelf life when paired with an aseptic filler and a sterilized downstream path.
How do you size a milk pasteurizer?
Divide the daily volume by the effective production hours (after cleaning and start-up), add 10–20% headroom, then size the holding tube for the required seconds at that flow. A 20,000-litre day processed in 8 effective hours needs about 2,500 L/h; a 3,000 L/h unit gives comfortable margin.
- Fix the daily volume and product mix (milk, cream, yogurt base) and the hours you can actually run.
- Subtract cleaning time. A heated circuit CIP with rinse, caustic, rinse and acid steps takes roughly 70–90 minutes.
- Calculate hourly flow and round up to the next standard capacity.
- Size the holding tube. The handbook's worked example: 10,000 L/h held for 15 seconds in a 48.5 mm tube needs about 26.5 m of holding tube.
- Check upstream and downstream matching with the separator, homogenizer and filler so the pasteurizer is not forced into frequent recirculation.
What should a pasteurizer specification include?
A complete specification states product, flow rate, inlet and outlet temperatures, pasteurization temperature and hold time, regeneration percentage, heating and cooling media, control and recording functions, and CIP requirements. Missing any of these makes supplier quotations impossible to compare.
- Safety controls: automatic flow diversion valve, independent temperature recording, pressure differential protection across regeneration.
- Hygienic design: AISI 304 or 316L product-contact stainless steel, food-grade gaskets, self-draining pipework.
- Heating medium: hot-water circuit (gentler, keeps the wall-to-product temperature difference to a few degrees and limits fouling) versus direct steam.
- Cooling: regeneration plus a chilled or ice-water section to reach about 4 °C.
- Cleaning: CIP-ready with acid and caustic steps, plus a 90–95 °C hot-water sterilization routine before production.
- Integration: homogenizer position, separator, deaerator and buffer tanks.
When we engineer a pasteurization skid, we start from these data points and the product's fouling behaviour, because a unit that is correctly sized for flow but not for run time will spend too much of the day in cleaning.
What are the most common buying mistakes?
The most frequent errors are buying on nominal capacity without allowing for cleaning time, choosing plates for products that foul or carry particles, skipping the booster pump or diversion valve, and planning UHT without budgeting for aseptic packaging. Each of these leads either to food-safety risk or to a line that never reaches its rated output.
If you would like a second opinion on your pasteurizer specification, our engineers can review your product mix and flow data and suggest a suitable configuration.
Frequently asked questions
What is the difference between HTST and UHT milk?
HTST milk is heated to at least 72 °C for 15 seconds and must be refrigerated, typically lasting 7–10 days. UHT milk is heated to 135–150 °C for a few seconds and filled aseptically, so it is commercially sterile and keeps for months at room temperature.
Is a plate or tubular pasteurizer better for milk?
For plain milk, a plate pasteurizer is usually better because it recovers up to about 95% of heat in a compact footprint. A tubular unit is better for viscous products, drinks with pulp or particles, very long runs, and indirect UHT, where higher pressures and temperatures are needed.
When does a batch pasteurizer make sense?
A batch (vat) pasteurizer makes sense for small volumes, frequent recipe changes, or cheese and yogurt making where the vat can also serve as a process tank. It holds milk at 63 °C for 30 minutes, so throughput is limited and energy recovery is minimal.
Why do pasteurizers need a flow diversion valve?
The flow diversion valve automatically sends milk back to the balance tank if it falls below the set pasteurization temperature at the end of the holding tube. It prevents under-processed milk from reaching the cooling section and filler, and is a core regulatory control point.
Sources
- IDFA – Pasteurization (time/temperature table from the PMO)
- Codex – Code of Hygienic Practice for Milk and Milk Products (CAC/RCP 57-2004)
- Tetra Pak Dairy Processing Handbook – Heat exchangers
- Tetra Pak Dairy Processing Handbook – Long-life dairy products
- Tetra Pak Dairy Processing Handbook – Pasteurized and ESL dairy products
- FDA – NCIMS Model Documents (Grade A Pasteurized Milk Ordinance)